
aluminum profile surface treatment additives help manufacturers control cleaning, surface appearance, oxide formation, coloring, and sealing. Their value depends on how well they fit the alloy, equipment, and required finish. An additive that performs well on one production line may need different operating conditions on another.
For buyers, selecting aluminum profile surface treatment additives involves more than comparing prices. The useful questions concern cleaning reliability, bath maintenance, chemical consumption, and finished product quality. This guide explains the main chemical categories, their functions, and practical ways to evaluate them before routine production.
Aluminum profile surface treatment additives are formulated products used to modify the performance of chemical treatment baths. Depending on their purpose, they may improve wetting, control foam, manage dissolved metal, stabilize coloring solutions, or support sealing. Some are separate concentrates; others are incorporated into complete treatment products.
The distinction matters when purchasing. An aluminum degreaser may be a complete cleaner, while a wetting additive supplements an existing formulation. Similarly, Aluminum anodizing chemicals include base electrolytes and auxiliary products. Buyers should establish whether a quotation covers a complete bath system, an additive package, or a replenishment concentrate.
A typical decorative anodizing route includes cleaning, rinsing, etching or brightening, desmutting, anodizing, optional coloring, and sealing. The actual sequence depends on the material and desired finish. Aluminum pretreatment establishes the condition of the metal before the oxide coating is formed.
Aluminum profile surface treatment additives should therefore be assessed as part of the whole sequence. A cleaner that leaves residues can affect later operations, while poor rinsing can transfer incompatible chemicals between tanks. Effective aluminum pretreatment requires compatible chemistry, suitable transfer times, and reliable rinsing throughout the line.
An aluminum degreaser removes oils, handling contamination, and other organic soils before subsequent treatment. Wetting agents help the solution contact the surface, while detergent components help release and disperse contamination. The formulation must match the actual soil rather than simply produce a visibly active bath.
Select an aluminum degreaser according to whether metal removal is acceptable. Bright or mechanically polished profiles may require a nonetching cleaner. Where a controlled matte finish follows, the cleaning requirements may differ. Acidic and alkaline products are both available, but their suitability depends on formulation and application.
Evaluate aluminum degreaser performance on representative profiles, including grooves and recessed areas. Inspect cleanliness after rinsing and check for staining or unwanted attack. A water break check can reveal uneven wetting, although it does not identify every contaminant. Compare aluminum degreaser results with downstream finish quality before approving a change.
Etching removes a controlled amount of aluminum to develop the required texture. alkaline etching commonly uses sodium hydroxide, while acidic processes offer different surface effects. Etching additives can influence bath behavior, appearance, drainage, and the management of dissolved aluminum, depending on the formulation.
For aluminum profile surface treatment additives used in etching, consistent appearance is a more useful target than maximum reaction speed. Excessive metal removal can affect dimensions and increase material loss. Etching additives cannot reliably conceal every extrusion defect, deep scratch, or variation associated with the underlying alloy.
Assess etching additives at realistic bath ages, rather than only in freshly prepared solutions. Record free alkali where applicable, dissolved aluminum, temperature, and treatment time. Compare texture and metal loss against an approved sample. These observations help determine whether etching additives remain effective as production loading changes.
After etching, alloy constituents can remain as a dark surface residue known as smut. Desmutting removes these residues, while deoxidizing addresses surface oxides. The functions can overlap in commercial products, but neither should be assumed to replace proper degreasing.
Aluminum pretreatment chemistry must suit the alloy being processed. Profiles with different alloy compositions may respond differently to the same bath. When reviewing aluminum profile surface treatment additives for this stage, request evidence of residue removal, compatibility with the selected etch, and minimal unwanted attack on the prepared surface.
Include rinsing in the evaluation of these aluminum anodizing chemicals. A profile that appears clean while wet may still carry residues into the next tank. Establish inspection points after aluminum pretreatment and investigate incomplete cleaning before adjusting the anodizing electrolyte. This avoids treating an upstream problem as an oxide formation problem.
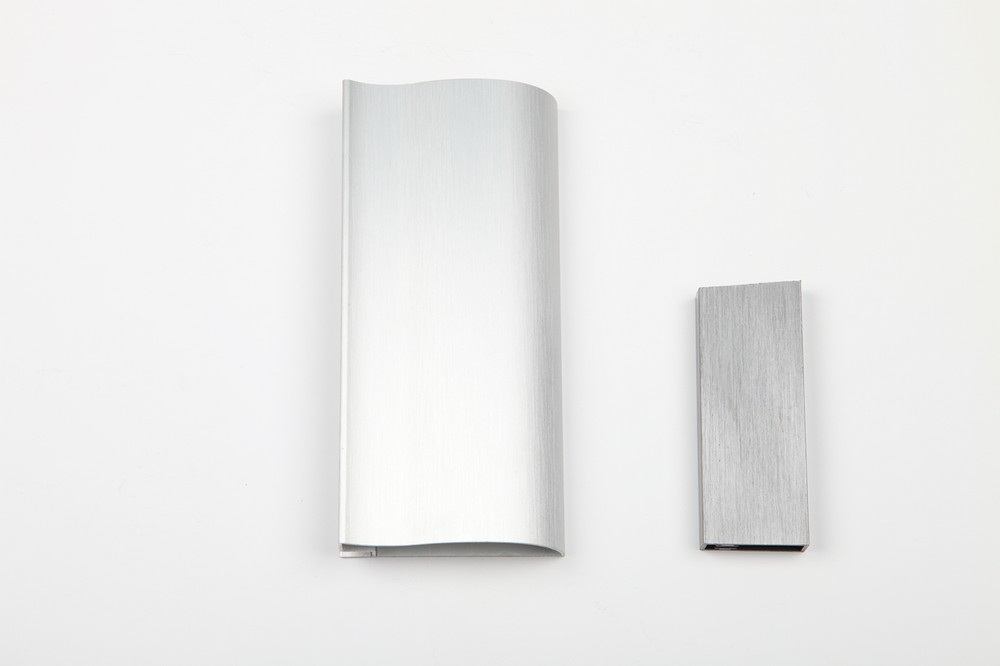
Anodizing uses electrical current to grow an oxide layer from the aluminum substrate. Aluminum anodizing chemicals provide the electrolyte environment in which this occurs. Selected anodizing additives may modify process behavior, but they must be evaluated within the intended electrolyte system and operating conditions.
Claims involving improved temperature tolerance or reduced cooling demand require production evidence. Anodizing additives do not eliminate the importance of electrical contact, current distribution, agitation, and heat removal. Compare aluminum anodizing chemicals using coating measurements and relevant performance tests, rather than judging a bath solely by processing speed.
Aluminum profile surface treatment additives also need a defined maintenance method. Ask how anodizing additives are measured and replenished, which contaminants matter, and what corrective actions are permitted. Avoid mixing unrelated additive packages without compatibility testing. Aluminum anodizing chemicals should be managed as a controlled formulation rather than an interchangeable collection of ingredients.
Coloring may involve dyes absorbed into the porous oxide or electrolytic deposition within the pores. Certain aluminum anodizing chemicals help maintain coloring bath stability. In appropriate electrolytic systems, coloring additives may help control metal salt stability and support more consistent deposition.
However, aluminum profile surface treatment additives cannot compensate for every source of shade variation. Alloy differences, surface texture, oxide thickness, and electrical conditions may all influence appearance. Keep reference samples and assess color under consistent lighting. Investigate the complete process when a shade drifts, rather than automatically increasing coloring additive dosage.
Sealing treats the porous anodic coating to improve its protective performance. Sealing additives differ according to the selected hot, intermediate temperature, or cold process. Their suitability also depends on whether the surface is clear, dyed, or electrolytically colored.
Choose sealing additives using the required finish specification and verified coating performance. A lower operating temperature may reduce heating demand, but total value also depends on treatment time, rinsing, bath maintenance, and any required aging. Nickel-free sealing additives are available, although their operating requirements remain formulation specific.
For aluminum profile surface treatment additives used in sealing, appearance alone is insufficient evidence of success. Check sealing quality with a test appropriate to the chemistry and applicable specification. Also inspect for deposits, haze, and color changes. Maintain sealing additives according to analytical results and production history, rather than adding product whenever a surface defect appears.
Start with the profile alloy, finish target, exposure conditions, and production method. Then list tank materials, heating capacity, agitation, filtration, and rinse arrangements. Surface treatment additives should fit these conditions without creating an unmanageable maintenance burden or disrupting established downstream operations.
Request technical data, safety information, analytical procedures, and replenishment guidance for each candidate. For an aluminum degreaser, ask about soil handling and rinsability. For etching additives, examine bath aging and metal loss. For aluminum anodizing chemicals, establish electrolyte compatibility and coating acceptance criteria before comparing commercial offers.
The most useful specification for aluminum profile surface treatment additives describes measurable results. Define acceptable appearance, cleanliness, coating thickness, color variation, and sealing performance as applicable. Confirm how deviations will be investigated and who will provide technical support. Clear acceptance criteria make supplier comparisons more meaningful than broad claims about quality or efficiency.
Application details also influence the purchasing decision. Window frames may place particular emphasis on visual agreement between adjacent components, while industrial assemblies may prioritize dimensions and specified coating properties. Long hollow sections require attention to drainage and trapped solutions. Define which surfaces will be visible and which dimensions are critical before requesting trial samples. This allows the proposed treatment to be assessed against the actual product rather than an ideal laboratory coupon.
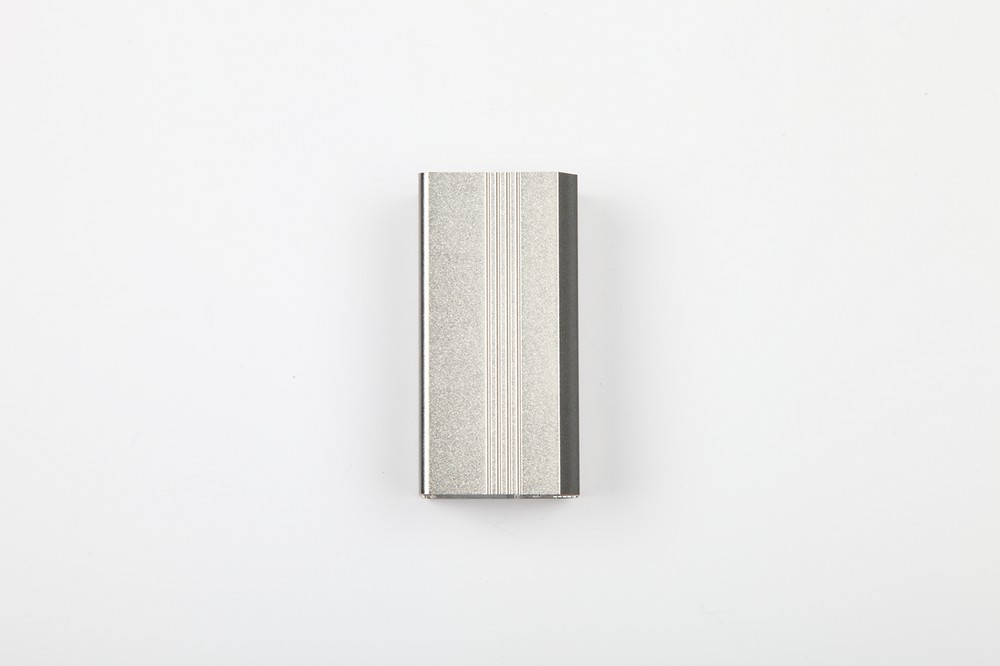
Stable results require stable operating conditions. Surface treatment additives should have defined concentration limits and a documented method of addition. Use chemical analysis where available, supported by workload records and inspections. A bath's color, foam level, or apparent activity is rarely enough to establish its composition.
Keep dosing records for aluminum degreaser, etching additives, and sealing additives alongside temperature and treatment time. Record abnormal events, such as extended shutdowns or unusually oily loads. Review aluminum anodizing chemicals on the same basis so that changes in finish quality can be compared with actual operating conditions.
Rinsing deserves equal attention during aluminum pretreatment. Profile orientation and drainage influence how much solution leaves each tank. Surface treatment additives with improved drainage may help in suitable applications, but they cannot replace adequate rinse design. Check rinse condition and carryover before assuming that higher additive concentration will improve results.
Create a simple response plan for measurements outside the approved range. State who checks the result, whether a second sample is required, and when production should pause for investigation. Keep measuring equipment suitable for the solution being tested and maintain its calibration. Consistent sampling locations and timing make trends easier to interpret than isolated readings collected under changing conditions.
When cleaning is uneven, inspect the incoming soil, aluminum degreaser condition, treatment time, and solution access to recessed areas. Check whether contamination is accumulating faster than the bath can manage it. Increasing aluminum degreaser dosage without identifying the cause may add cost while leaving the underlying problem unresolved.
For inconsistent matte appearance, review alloy batches, surface condition, etching additives, bath analysis, and temperature distribution. For color variation, compare oxide thickness, rack position, and coloring conditions. Aluminum anodizing chemicals may contribute to a defect, but investigation should also include electrical contact and earlier aluminum pretreatment stages.
When haze or deposits appear after sealing, inspect rinse contamination, sealing additives, bath condition, and operating time. Surface treatment additives should be adjusted only after checking the relevant control data. Change one controllable factor at a time where practical, and retain samples so that the effect of each correction remains visible.
Compare aluminum profile surface treatment additives by cost per accepted production unit, not simply price per container. Include chemical consumption, metal loss, heating, water use, maintenance, waste treatment, and rejected work. A concentrated product may have a different working cost from a cheaper, more dilute alternative.
Run trials using representative alloys, profile geometries, contamination levels, and finish requirements. Compare the proposed surface treatment additives with the existing process under documented conditions. Include fresh and aged bath behavior where feasible. Evaluate aluminum degreaser cleanliness, etching additives performance, and sealing additives results using the same acceptance criteria.
Before full adoption, confirm that aluminum anodizing chemicals can be analyzed and maintained by the production team. Establish a baseline for consumption and rejected work, then review results over several production cycles. A successful trial should demonstrate repeatability and manageable process control, rather than produce only one attractive sample.
Agree on the trial report before starting. Record the treated area, accepted quantity, product additions, processing time, and reasons for rejection. Photograph comparison samples under the same lighting and retain physical references where possible. Discuss any change in waste handling or maintenance workload with the responsible team. These records give purchasing, production, and quality staff a shared basis for deciding whether the proposed change delivers a practical improvement. Repeat the comparison when incoming material or production conditions differ substantially from the trial.
Generally, each stage has different chemical requirements. Surface treatment additives designed for an alkaline cleaner should not be treated as substitutes for anodizing additives or sealing additives. Some products combine functions within a specific stage, but compatibility must be established for the intended process.
Not necessarily. Excess aluminum degreaser may increase rinsing demand, while excessive etching additives or other chemicals may disturb bath balance. Follow the validated operating range and investigate contamination, temperature, and treatment time before increasing concentration. More product is not a reliable substitute for process diagnosis.
Provide the alloy, profile geometry, finish target, process sequence, bath analysis, operating conditions, and examples of the problem. This helps identify suitable aluminum profile surface treatment additives and relevant trial conditions. Select aluminum anodizing chemicals through documented testing, and maintain aluminum pretreatment with records that connect bath condition to finished quality.
邮箱

本网站使用 cookie 来确保您在我们的网站上获得最佳体验。

 English


 Whatsapp
 电话
 邮箱
 留言
评论
(0)